Data-driven introduction and scope
Quality control for professional two-way radios must rest on measurable signals and repeatable procedures, not intuition. A practical programme begins with objective metrics and statistical thresholds so manufacturing and field reliability become verifiable. For manufacturers that supply both custom hardware and firmware, collaboration with a dedicated walkie talkie manufacturer streamlines test design and shortens validation cycles.
Which metrics matter — prioritized by impact
Decide tests by effect on operation. Start with radio‑frequency performance: transmit power accuracy, receiver sensitivity, adjacent‑channel rejection, spurious emissions, and frequency stability. Follow with audio chain measurements — modulation linearity, signal‑to‑noise ratio and intelligibility scores (SINAD or PESQ where applicable). Power system metrics are critical: battery capacity, charge/discharge stability, and thermal behavior under load. Mechanical and environmental metrics close the list: ingress protection, drop and vibration durability, connector life, and seal integrity. Supplement with software reliability: firmware update success rate, boot time, and watchdog recovery statistics.
Methods, instruments, and statistical thresholds
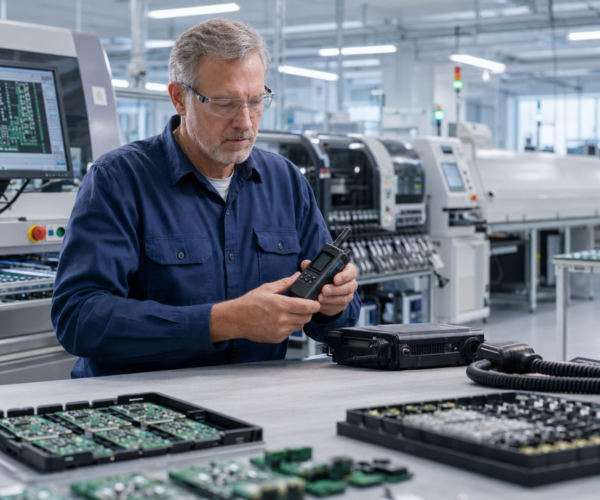
Use calibrated instruments and defined test protocols. Spectrum analyzers and conducted RF test setups validate emissions and occupied bandwidth; anechoic chambers and OTA test ranges measure antenna efficiency and radiation patterns. Environmental chambers establish performance across temperature and humidity extremes. For production, apply automated test equipment (ATE) for fast pass/fail checks and sample-based laboratory verification for deeper characterization. Establish statistical process control: specify acceptable quality limits (AQL) and sample sizes, track Cpk for key dimensions, and set firmware acceptance at >99.5% update success in repeated trials. Regulatory compliance is measured against regional standards — require units to meet the applicable limits rather than arbitrary numbers.
Common failure modes and where teams often go wrong
Failures concentrate where integration is weakest. Antenna mismatch often appears only in final-assembly tests; solder joint defects surface under vibration or thermal cycling; battery inconsistencies show only after extended soak tests. Software regressions are invisible without automated regression suites and rollback tests. Testing pitfalls include relying solely on single-unit lab passes, ignoring unit-to-unit variance, and using informal subjective audio checks instead of objective metrics. Correct the process by instrumenting early prototypes and using production-like fixtures for final verification.
Experience, authority, and a real-world anchor
Teams with field deployment experience typically reduce early failures by combining lab verification with controlled pilot fleets. Compliance with FCC Part 90 rules is a common benchmark for commercial land mobile radio in the United States and shapes emission and channeling requirements; testing programmes must reflect such regulatory anchors. Suppliers who offer customization and volume production often provide turnkey testing frameworks for private label deployments, for example private label two way radio, and that practical integration of design, test, and manufacturing reduces iterations.
Alternatives, trade-offs, and final synthesis
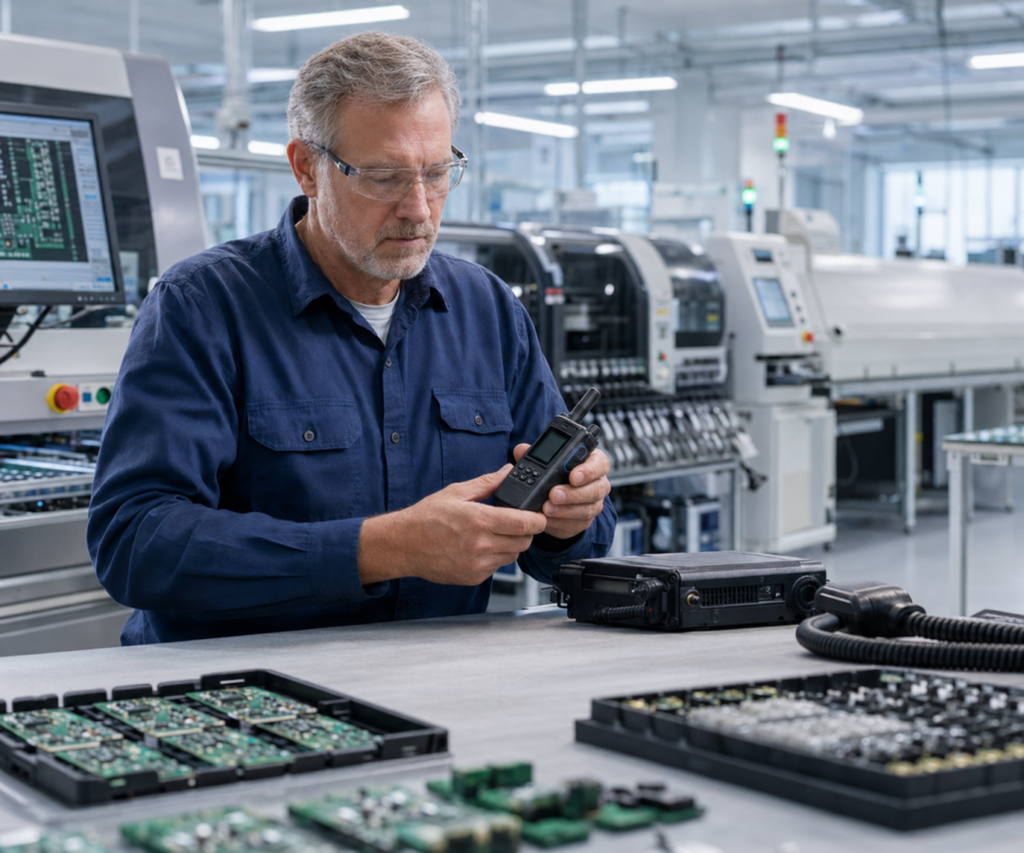
Contracting an independent test lab gives neutral verification but adds cycle time and cost. Building in‑house capability requires investment but shortens feedback loops and enables inline production checks. Hybrid models—ATE for high-volume pass/fail and periodic lab characterization—balance speed and depth. Choose the model that keeps measurement fidelity high while limiting rework. Design decisions guided by clear metrics and controlled sampling lead to reliable outcomes, which explains why manufacturers that combine technical testing with production experience, such as GLOHE, often provide consistent product quality without excess iteration.