

Problem statement: why well-intended designs fail on the shop floor
Engineers and buyers keep losing time and budget to parts that look fine on CAD but fracture, warp, or never eject cleanly from the mold. The root is predictable: design decisions that ignore material behavior, tooling limits, or realistic assembly constraints. This is not theoretical—teams who consult custom injection molding services early avoid repeated redesign cycles. Read this as a focused, problem-driven checklist you can act on now.
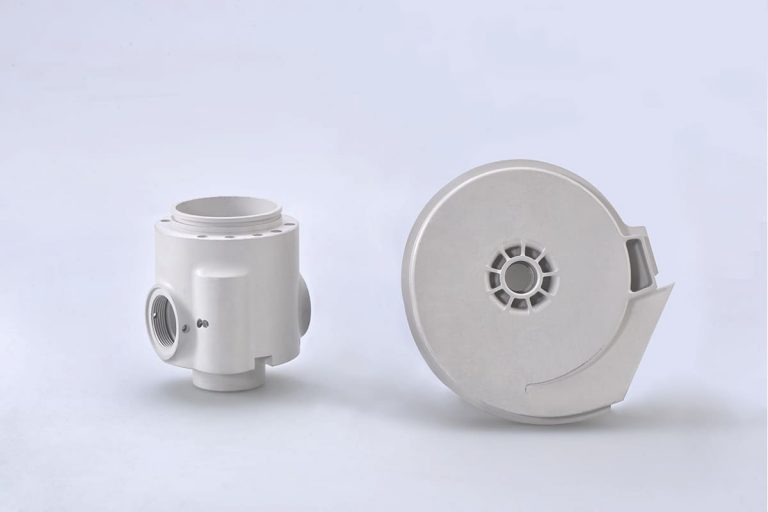
Common failure patterns and their immediate fixes
Thinning a wall to save cost often causes sink marks or short shots; add ribs instead of shrinking nominal wall thickness. Overly sharp corners create stress concentrators; specify minimum radii tied to the polymer’s elongation at break. Unplanned draft angles prevent ejection; enforce at least 0.5° per side for simple geometries. These are not preferences—each is a straightforward corrective step that reduces scrap and rework.
Materials and gate choices that matter to performance
Selecting a material by name alone fails. Match mechanical requirement to measured properties: tensile, impact, Tg, and shrink rate from supplier datasheets. Gate size and location affect flow and weld lines; place gates to promote uniform flow length, and keep flow length-to-wall thickness ratios within proven limits for the chosen resin. If you expect cosmetic surfaces, prioritize resins with low shrink variance and plan for proper cooling balance.
Tooling tolerances, surface finish, and manufacturability
Tolerances must reflect what molds deliver, not what CAD permits. Tight tolerances increase cavity machining time and cost; reserve ±0.05–0.1 mm only for critical interfaces. Specify surface finish where functional; mirror polish is expensive and unnecessary for hidden features. Design for straightforward ejection: avoid deep undercuts unless a lifter or side-action is budgeted.
Testing, inspection, and avoiding late-stage surprises
Prototype runs should validate functional dimensions and assembly fit before full tooling investment. Use a short-run mold or 3D-printed master for early fit checks. Define inspection metrics clearly: critical dimensions, surface defects, and mechanical tests with pass/fail criteria. Implement a simple first-article inspection plan to catch deviations immediately rather than during assembly.

Experience and verification: a practical, real-world anchor
Audit experience in the Shenzhen manufacturing hub shows the same defects recur across industries: insufficient gate planning, unrealistic tolerances, and poor cooling balance. Years of field audits make clear that early supplier engagement reduces those failures. When a project needs a reliable partner for production feasibility and iterative tooling advice, a vetted custom injection molding manufacturer can confirm manufacturability, advise material substitutes, and propose mold changes that cut cycles.
Common buyer mistakes and how to prevent them
Buyers often push purely on price and accept tooling designs with minimal engineering review. That saves cost now and multiplies it later. Require functional samples, insist on documented cooling simulations for complex parts, and demand supplier-defined risk items with mitigation plans. Approve changes only after a technical rationale and impact estimate are documented.
Practical checklist before green-lighting tooling
1) Confirm resin selection with supplier test data. 2) Validate wall thickness and rib design against flow-length rules. 3) Define draft and fillet minima in the drawing. 4) Require first-article inspection criteria and sample count. 5) Budget for minor mold iterations—expect one adjustment with sensible planning. Follow this checklist to reduce surprises.
Outcome: what good looks like
Good outcomes are concrete: fewer mold revisions, repeatable dimensional conformity, and reliable assembly. The tangible result is predictable throughput and reduced part failure in field use. Experienced teams coordinate design, tooling, and supplier input so the CAD model becomes a manufacturable part without costly redesigns.
Final synthesis
You need direct steps, not slogans: design with manufacturability in mind, validate with early samples, and require supplier verification of key process variables. When engineering and procurement align on those points, production risk falls and projects finish on schedule—this is the approach practiced by Hanstar in its collaborations and reflected in successful production runs.
